


The simplest, highest-value way to track scrap by cause is to record every scrap event at the workstation with a short standard cause code plus the weight or quantity. This single habit turns scattered waste into a prioritised list of improvement opportunities, because once reasons are coded consistently, you can see exactly where cost and material are leaking.
TL;DR:
- Direct weighing paired with cause codes gives a reliable baseline, but reserve it for high value or high volume lines because it takes operator time.
- Use six to ten cause groups with optional subcodes, but keep the entry screen to eight or fewer choices and preselect the most common cause.
- Review weekly Pareto charts of scrap cost, investigate the leading cause with a named owner, and record whether defects should be reworked or scrapped.
- A focused pilot can produce a useful Pareto chart in 30 to 90 days; track unspecified entries to check whether the taxonomy is working.
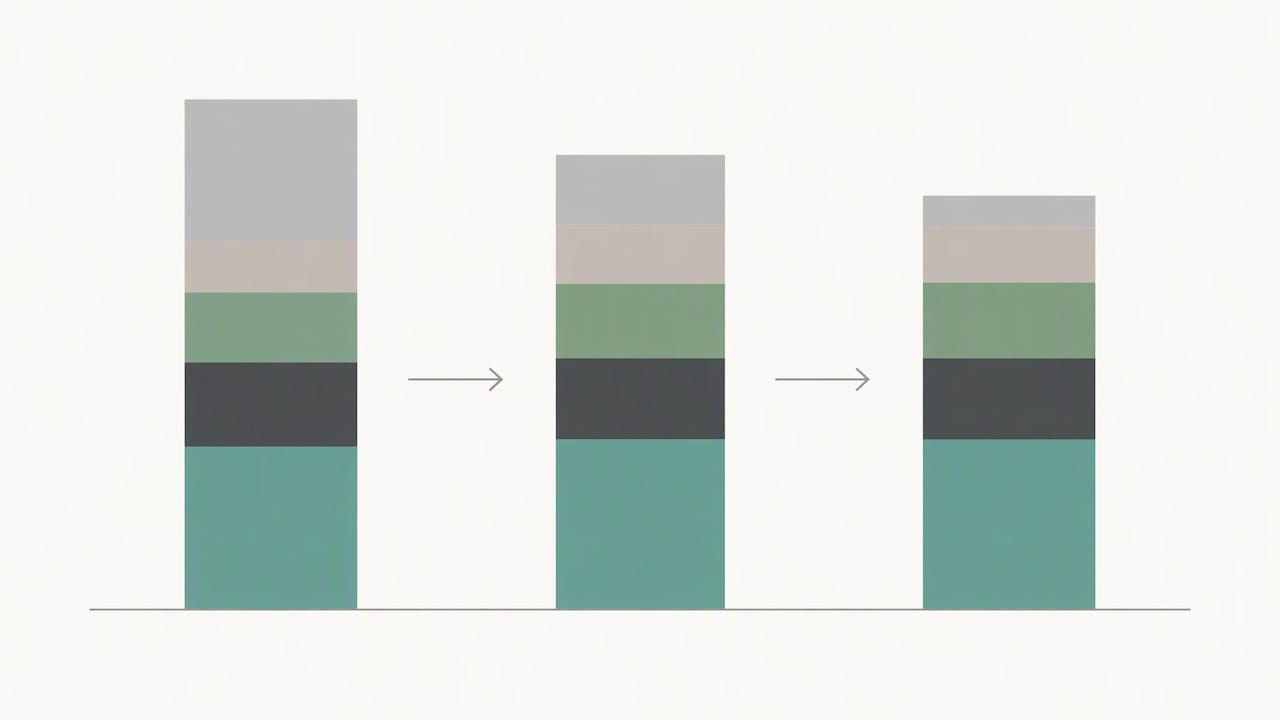
- A factory case study cut unspecified scrap reasons from over half to just over a tenth after grouping causes and defining rework workflows, without new equipment.
Without cause codes, scrap becomes an anecdote. Operators remember the big spill, not the dozens of small setup errors that add up to more cost over a month. Structured recording changes that: when reasons are logged alongside quantity, a factory in the metal-mechanical sector cut unspecified scrap reasons from over half to just over a tenth and recorded measurable cost savings within months after grouping reasons and building a consistent workflow around them, according to a systematic classification study.
This data feeds directly into the KPIs you already track:
Capture method matters as much as the taxonomy itself. Practical guidance on measuring loss recommends starting with a clear business case, defining scope and pairing direct weighing with cause logging wherever weighing is feasible, because weight-based measurement is the most reliable baseline available on a production line.
In order of typical adoption:
Pro Tip: Keep the on-screen code list to eight or fewer entries with the most frequent cause pre-selected as the default; operators who have to scroll or think twice will skip the step under pressure.
Reducing the burden on operators is what decides whether this data collection survives past the first week. A short code list, sensible defaults and a brief sampling protocol for lower-value lines all keep logging fast enough to stick.
A taxonomy only works if operators actually use it, which means the primary list has to stay short. Six to ten primary categories, each with optional subcodes for detail, tends to cover most factories without overwhelming the entry screen.
This grouping discipline is exactly what let the metal-mechanical case study bring unspecified reasons down from over half of all scrap to just over a tenth, a shift that came from electronic grouping and defined rework workflows rather than from new equipment.
Once causes are coded consistently, the analysis follows a familiar quality-management sequence. Track scrap rate by cause, cost by cause and the percentage still falling into “unspecified” as your three headline KPIs, then apply ISO 22400’s KPI definitions to keep the formulas consistent across lines and shifts, which matters once you start comparing performance between cells.
A short pilot focused on one line and a small code list typically produces the first useful Pareto chart within 30 to 90 days, according to practical measurement guidance, and that early visibility is usually what convinces a plant to extend the programme to other lines.
Measuring improvement is straightforward once the baseline exists: compare cost by cause month over month and watch the unspecified percentage fall as the taxonomy matures. Our guide to cutting rework walks through this RCA and SPC combination in more detail for a single pilot line.
Most pilots follow a similar arc. Here is a workable 30 to 90 day sequence:
A connected MES removes much of the manual overhead in this sequence: configurable cause codes, automatic linking of scrap events to machine and operator, and live dashboards mean fewer missed entries and faster weekly reviews.
Pro Tip: Measure success in weeks nine to twelve by the drop in your unspecified percentage, not just by total scrap volume, since that figure tells you whether the taxonomy itself is working.
Start small. One line, one short code list and a two-week sampling check will tell you more than a factory-wide rollout that nobody maintains. Get a named sponsor and a single KPI everyone watches, then use the first Pareto chart and its early cost savings to justify budget for barcode capture or automated weighing later. Protecting operator time matters more than taxonomy elegance in the first month.
— Andraž
Once a pilot proves the approach, the manual side of this work becomes the bottleneck: typing codes into a spreadsheet, chasing missing entries, rebuilding Pareto charts by hand. That is the gap a connected MES is built to close.
We built Mestric™ MES around this kind of real-time capture and analysis, and we offer a demonstration where you can see connected equipment feeding live scrap and quality data on an actual production line. If scrap-by-cause tracking is on your list for this quarter, that demo is a practical next step before committing to any particular capture method.
Record the quantity or weight, the workstation, a timestamp and a short standard cause code at minimum. Direct weighing paired with cause logging is the most reliable combination according to practical measurement guidance.
Keep the primary list to around six to ten groups such as material, machine, process, tooling, human and specification, with optional subcodes for detail. An FMEA workshop is a practical way to populate that list before launch.
A focused pilot on one line with a short code list usually produces a first useful Pareto chart within 30 to 90 days, based on practical measurement guidance. That early result is normally what justifies extending the approach to further lines.
Yes. A connected MES can capture cause codes at the workstation, link them automatically to machine and operator, and update dashboards in real time, which cuts the manual entry and reconciliation that slow down spreadsheet-based tracking.
Watch scrap rate by cause, cost of scrap by cause and the percentage still logged as unspecified. ISO 22400 gives standard formulas for framing these KPIs consistently across lines.


 069 763 552