

A digital twin in manufacturing is a virtual model of a machine, line or process that stays synchronised with the real one through live data. It is not a 3D drawing and not a one-off simulation. It only becomes useful once reliable data flows from your shop floor into the model. For most plants, that data foundation is the real starting point, and it is where you can make progress this quarter.
This guide explains what a digital twin is, how it connects to equipment, where it pays off, what Slovenian projects have reported and how to start without a multi-million budget.
NIST describes a digital twin as an integrated model that represents, connects and synchronises part or all of a physical manufacturing system or process, using historical and real-time data. The same NIST paper notes that simulations imitate operations, but most run standalone, without a direct link to real systems.
The ISA breaks the idea into three levels of data integration:
| Level | Data flow | Typical factory example |
|---|---|---|
| Digital model | No automated exchange; data is entered by hand | A layout or flow model built in simulation software |
| Digital shadow | One-way automatic flow, physical to digital | A live dashboard that mirrors line status and counts |
| Digital twin | Two-way automatic flow | A model that sends updated control parameters back to the machine |
Most plants that say they have a twin are at the shadow stage. That is a perfectly good place to be. The model is already fed by real data, and you can add feedback to the machines later.
One more distinction matters for planning. Shao and Helu note that an offline digital twin connects to the physical system periodically rather than continuously. That periodic link is what separates it from a traditional simulation model. So a twin does not have to run at millisecond speed to be worth building. A twin for production planning may refresh every shift.
NIST’s Simon Taylor adds a useful point of view: the most important attribute of a twin is that it represents the behaviour of the system. Connecting and synchronising are the means to that end. The aim is to make decisions faster and more agile, not to make the model look clever.
IEEE describes a twin system in three layers:
NIST’s standardised approach uses similar logic. It describes an observable manufacturing domain (people, equipment, material, processes), a device communication domain for data exchange and synchronisation, and the digital twin domain, which hosts the models and the analytics, simulation and optimisation services.
The middle layer is where most projects stall. Plants run machines from different decades and vendors. Some have modern controllers, others have only a signal tower and a counter. If you cannot get a stable stream of cycle counts, stoppage reasons and quality values out of the machine, the best model will show you fiction.
That is why we point plant engineers to the connectivity question first. Our guides on the role of IoT in manufacturing and on IoT gateways in manufacturing cover the hardware and protocol side. If your fleet includes older equipment, our page on connecting legacy machines describes how a pilot with one to three machines works.
Fraunhofer lists use cases across the whole value chain: product planning and development, production planning, production and assembly, logistics, maintenance and service, disassembly and recycling. For a plant manager, four are the most practical:
A twin also helps you present the factory. Photorealistic models are useful for explaining a line to management and customers, and a guide on 3D visualisation for manufacturers shows what to expect from that work. Visualisation is the presentation layer, though. The value for operations comes from the live data behind it.
Be careful with headline numbers. Each figure below comes from a specific project with its own baseline, and your results will depend on your starting point.
Two Slovenian projects show what this looks like locally.
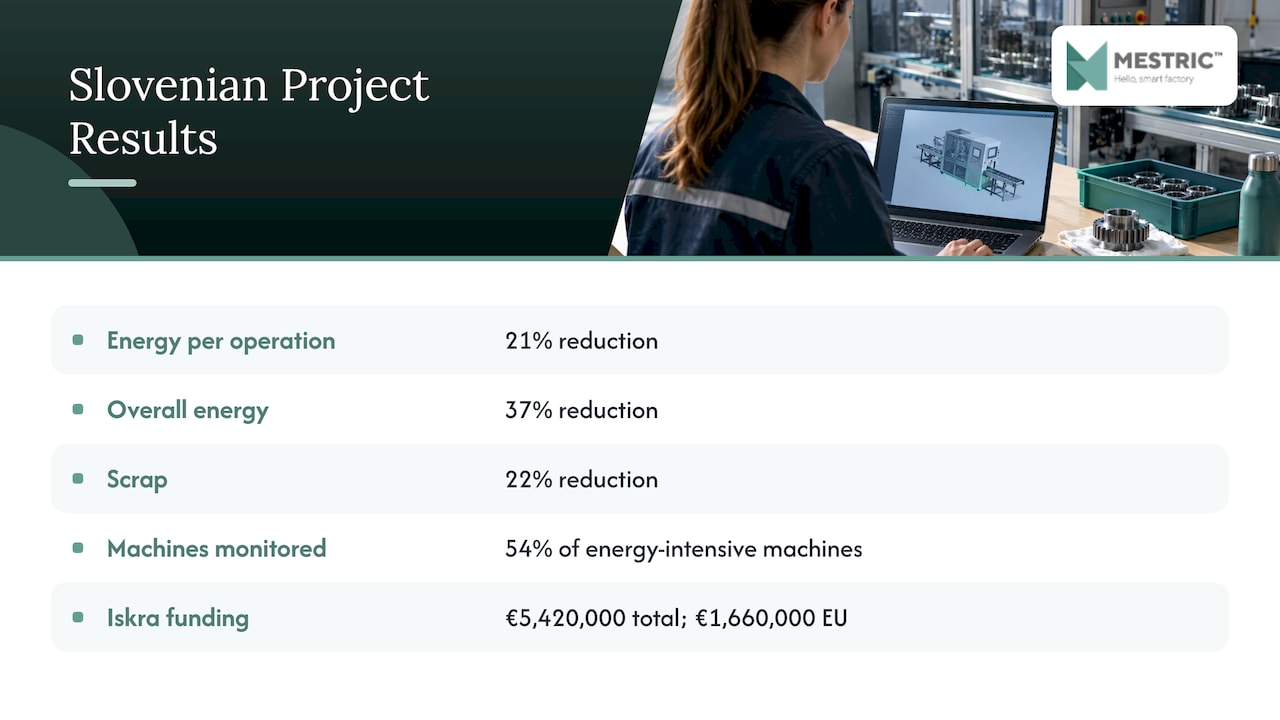
Gorenje Orodjarna took part in the DENiM project. It linked MODBUS energy and air-consumption sensors with ERP production data, built an energy dashboard and a machine-learning prediction pipeline, and used an AI tool for machine selection. The company reports a 21% electrical energy reduction per operation, a 37% overall energy reduction and a 22% scrap reduction, with 54% of energy-intensive machines monitored.
Iskraemeco ran the DT4DL project from April 2022 to March 2024. Its total value was €5,420,000, of which €1,660,000 was co-financed with European funds. The project covered digital twins for production and knowledge, AI decision support, IoT data capture, analytics and AR/VR. Miha Kern, Director of Manufacturing Engineering and Production, said it contributed to better traceability, real-time insight and fewer errors and unnecessary stoppages, and strengthened employees’ digital skills.
Notice what both projects share: sensor and production data connected to a model, then used for a concrete decision. Neither started with software alone.
You need machine states, cycle counts, stoppage reasons, quality parameters and order data in one place, collected automatically. Manual entry is too slow and too error-prone to keep a twin synchronised. Our article on the role of data in manufacturing covers data types and collection methods in more detail.
Timperi et al. identify four competence groups: technological skills (IT, programming, simulation, installation, plus mechanics, electricity and hydraulics), cognitive skills (analysis, problem-solving), soft skills (collaboration, curiosity) and managerial skills (supply chain and operations knowledge). They also argue that ownership of the twin, the core competence to maintain and fine-tune it, and the ability to lead development must sit inside the company. In practice, name one production owner and one technical owner early.
In a Slovenian pilot reported under the Inno2Mare programme, the parties agreed that the twin would not include sensitive data such as details of faulty parts. Each production line acted as a black box, focused on order numbers and energy consumption, and data moved over a secure VPN. Deciding what the twin may see is a sensible first governance step.
A review of twins at different manufacturing levels points to high initial costs and data-integration problems at line level, model complexity and cybersecurity risks at facility level, and oversimplification and organisational obstacles at enterprise level. Another study lists integration, investment cost, cybersecurity and a shortage of skilled people as the main hurdles.
The planning answer to each is the same: keep the first scope small.
The Singapore IMDA playbook offers a clear structure, and it applies well to a mid-sized plant. It recommends anchoring the twin to outcomes, starting with one or two priority use cases and a two-stage rollout.
The playbook’s readiness test for Stage 2 is practical: at least 4 to 8 weeks of stable data, agreed baseline KPIs and users confirming that dashboards are accurate enough to use in discussions.
When the first line works, scaling is a matter of repeating the pattern. A general guide on how to scale up manufacturing is a helpful companion for the capacity and process side of that step.
Most of the digital twin conversations we hear begin with the model and end with a data problem. The plant buys or builds a clever representation, then discovers that machine states, stoppage reasons and quality values are still written on paper or typed in at the end of a shift.
We think the order should be reversed. Capture the data automatically first, from the machines you already have. Show it live to the people who run the line. Agree the KPIs: performance, downtime, quality parameters and cost. Only then does a model have something true to mirror.
That is how we designed Mestric. It connects directly to production equipment, collects data automatically and presents live KPIs to production managers, with AI-powered tools that point to bottlenecks and process improvements. For many plants, that is the shadow stage of a digital twin, and it pays back in fewer manual errors and faster decisions long before any advanced modelling begins.
If you plan a twin, plan the data layer with the same care as the model. That is where we can help.
Andraž
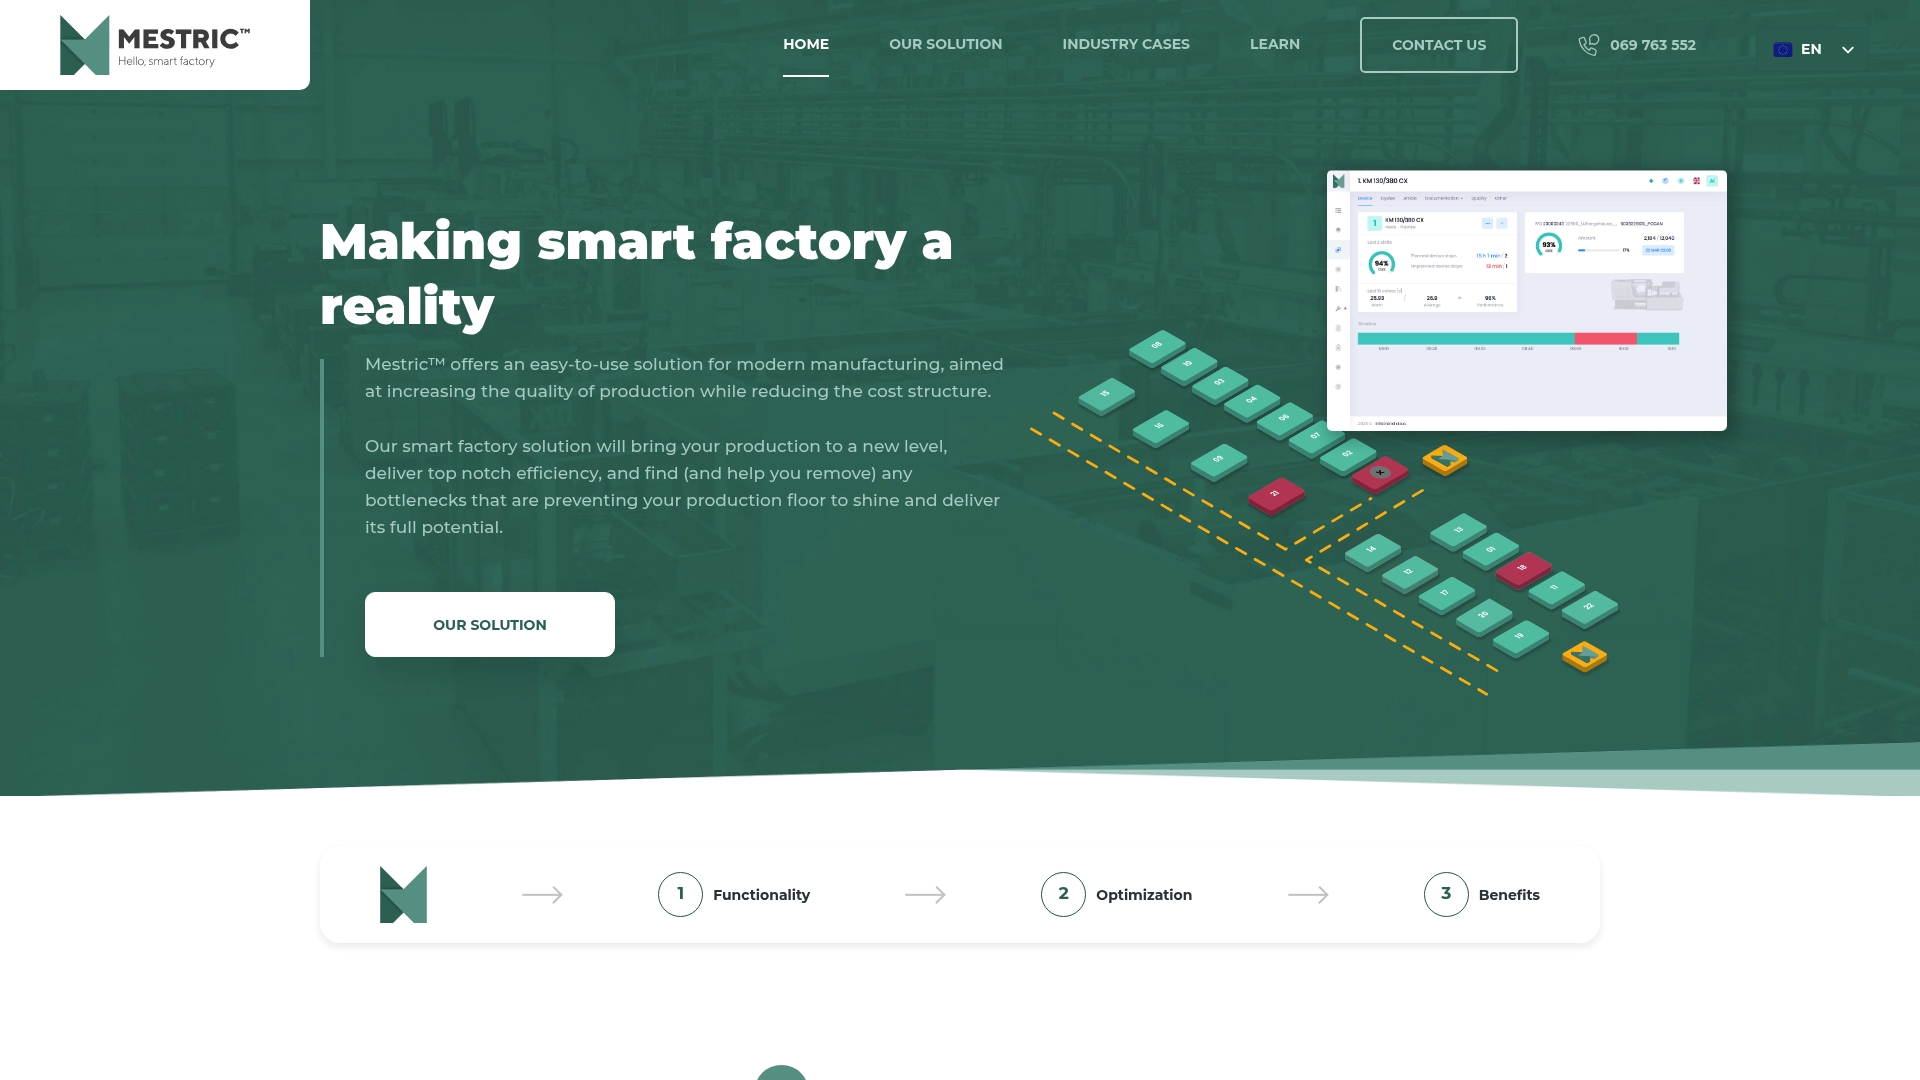
Mestric™ MES connects to your equipment, captures production data automatically and shows performance, downtime, quality and cost KPIs in real time. It gives you the live data layer a digital twin depends on, and you can see it working in a real production environment at our demo centre.
Read more on the Mestric™ MES solution page, or see how real-time production monitoring changes day-to-day decisions on the shop floor.
A simulation imitates a process and usually runs standalone, using data you enter. A digital twin is connected to the physical system and updated with its data, so it reflects the current state of the line. In the ISA classification, a twin also exchanges data in both directions, while a shadow only receives it.
No. Live machine data, KPI dashboards and downtime analysis deliver value on their own, because they show where output and quality are lost. They also give any later twin the stable data it needs. The IMDA playbook describes this as the first stage of rollout.
The IMDA playbook suggests at least 4 to 8 weeks of stable data and agreed baseline KPIs before adding predictive analytics and what-if simulation. The first stage, connecting core signals and building simple dashboards, can start with one line. Timelines depend on how many machines you connect and their condition.
IEEE names MQTT, OPC-UA and industrial buses as common ways to transport readings. Slovenian projects have also used MODBUS sensors, as in the Gorenje Orodjarna project. Older machines can often be connected through a gateway, so replacing equipment is not usually the first step.
Research on twin competences says ownership, maintenance skills and the ability to lead development should be inside the company. In practice, that means a production owner who defines the decisions and KPIs, and a technical owner who looks after data and models.


 069 763 552